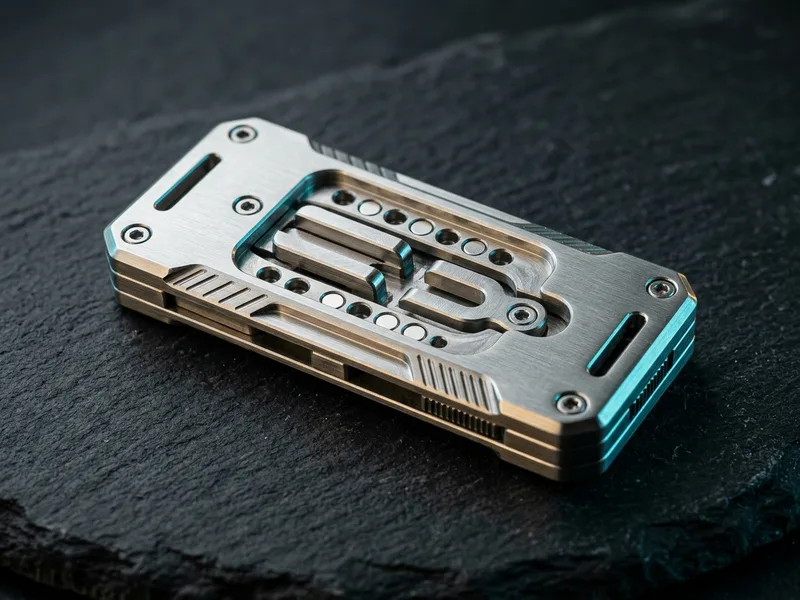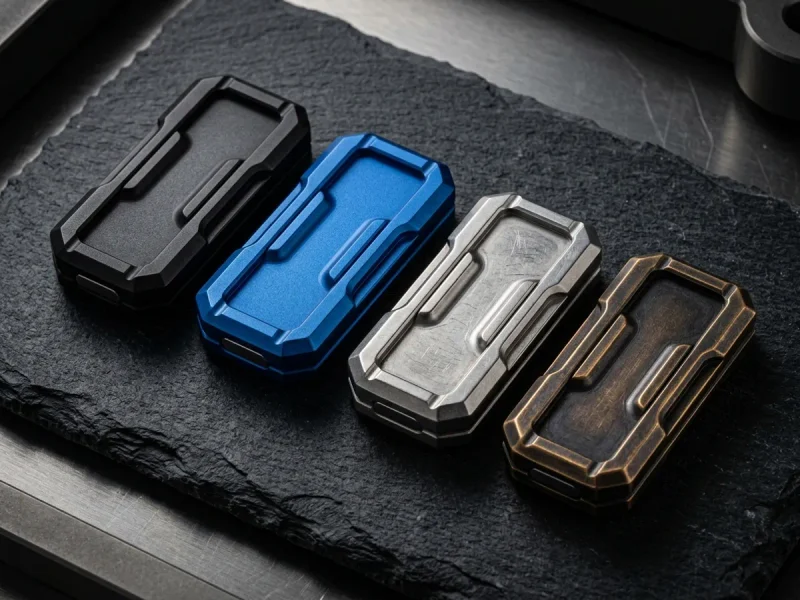
1. Why Surface Metallurgy Determines Whether an EDC Fidget Ages Like a Luxury Watch or Peels in 30 Days
An everyday carry (EDC) fidget slider, coin, or spinner endures one of the harshest tribological environments of any consumer product: 2,000+ thumb cycles per day, constant exposure to human palmar sweat (pH 4.5–6.8 with sodium chloride and lactic acid), and direct pocket abrasion against steel house keys and titanium pocket-knife clips.
If a supplier sprays cheap wet lacquer or single-layer flash plating onto a metal shell, the finish will blister, flake, or rub down to bare gray metal within three weeks.
Across our 140 factory molds (detailed in our Zinc Alloy vs. CNC Stainless Steel Cost Guide), we match every base alloy—Zamak #3 Zinc Alloy, 6063-T6 Aerospace Aluminum, 304/316 Stainless Steel, and Zr702 Zirconium—with industrial surface treatments engineered to pass 48-to-96 hour ASTM B117 neutral salt-spray and artificial perspiration testing.
2. Complete 5-Finish Surface Engineering Matrix: Hardness, Thickness & Sweat Resistance
Use the engineering specification table below to compare our five factory surface finishing processes across surface hardness (Vickers HV), coating thickness, pocket-scratch concealment, and custom logo compatibility:
| Surface Finishing Process | Compatible Base Alloys | Layer Thickness & Vickers Hardness | ASTM B117 Salt-Spray & Sweat Rating | Pocket-Scratch Concealment | Representative Production SKUs |
|---|---|---|---|---|---|
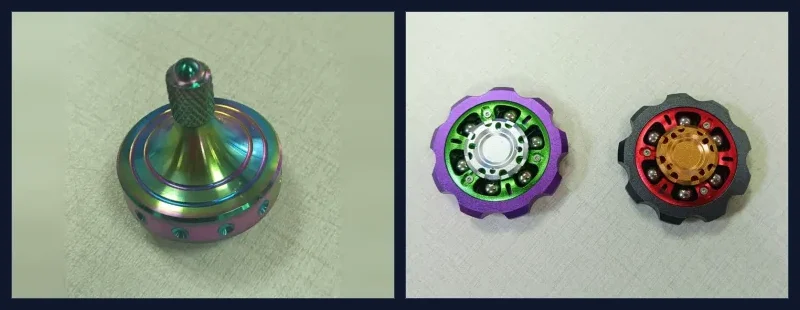
| 1. Vacuum PVD (TiN / ZrN / DLC / Rainbow) | 304 / 316 Stainless Steel & High-Grade Alloy | 1.5 – 3.5 μm · 1,800 – 2,400 HV | 96+ Hours (Impervious to sweat & acid) | 9.5 / 10 (Ultra-hard ceramic film resists key scratches) | FS-120, FS-144, FS-148 |
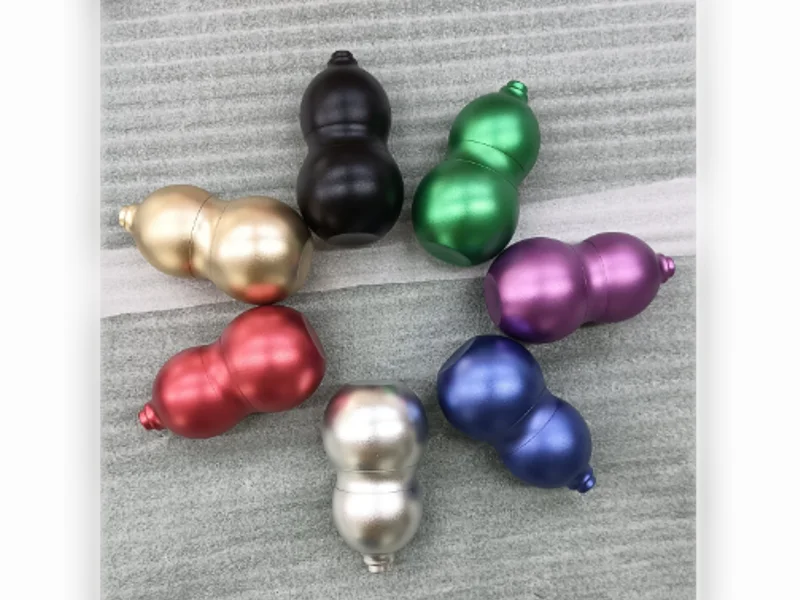
| 2. Type-II & Type-III Sulfuric Anodizing | 6063-T6 / 7075 CNC Aluminum Alloy | 15 – 35 μm · 350 – 500 HV (Integral $\text{Al}_2\text{O}_3$) | 72+ Hours (Sealed anodic pores) | 8.5 / 10 (Bead-blasted matte texture hides micro-wear) | FS-012, FS-047, FS-064, FS-096, FS-097 |
| 3. Ceramic Media Stonewash & Satin Brush | 303 / 304 / 316 CNC Stainless Steel | Bare Metal Passivated (`Cr2O3` film) · 200 – 240 HV | 96+ Hours (Surgical-grade corrosion immunity) | 10 / 10 (Isotropic matte tumble pattern makes new scratches invisible) | FS-005, FS-013, FS-063, FS-075, FS-086 |
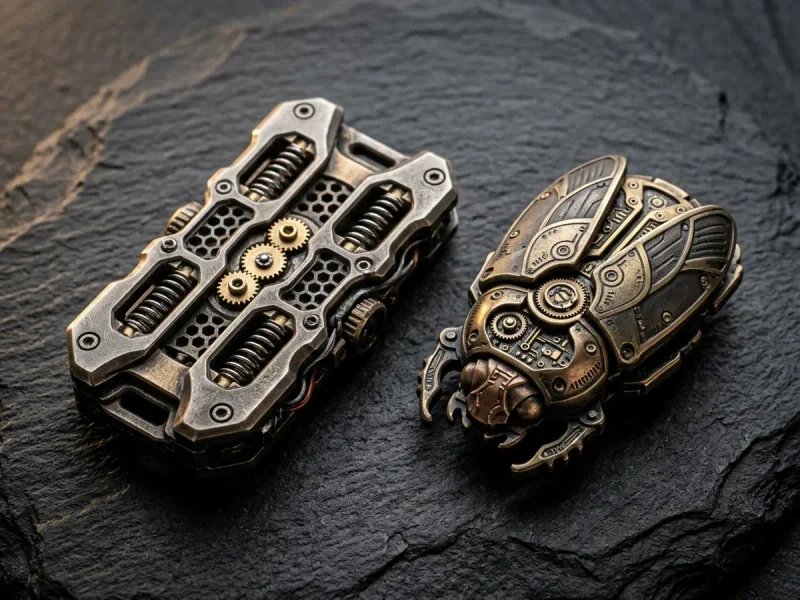
| 4. Relieved Antique Bronze / Silver / Gunmetal | Zamak #3 Die-Cast Zinc Alloy & Brass | 12 – 20 μm (Cu-Ni base + antique patina + electrophoretic clear coat) | 48+ Hours (Locked under bake-cured electrophoretic seal) | 9.5 / 10 (Dark recessed valleys + brushed high-spots age naturally) | FS-001, FS-010, FS-017, FS-023, FS-125 |
| 5. Thermal Flame Oxidation (`600°C`) | Zr702 Exotic CNC Zirconium | 5 – 12 μm · 1,200+ HV (Natural $\text{ZrO}_2$ black ceramic skin) | 100+ Hours (Chemically inert aerospace oxide) | 9.5 / 10 (Self-passivating obsidian ceramic surface) | FS-107, FS-114 |
3. How 4-Stage Relieved Antique Electroplating Brings 3D Sculpted Molds to Life
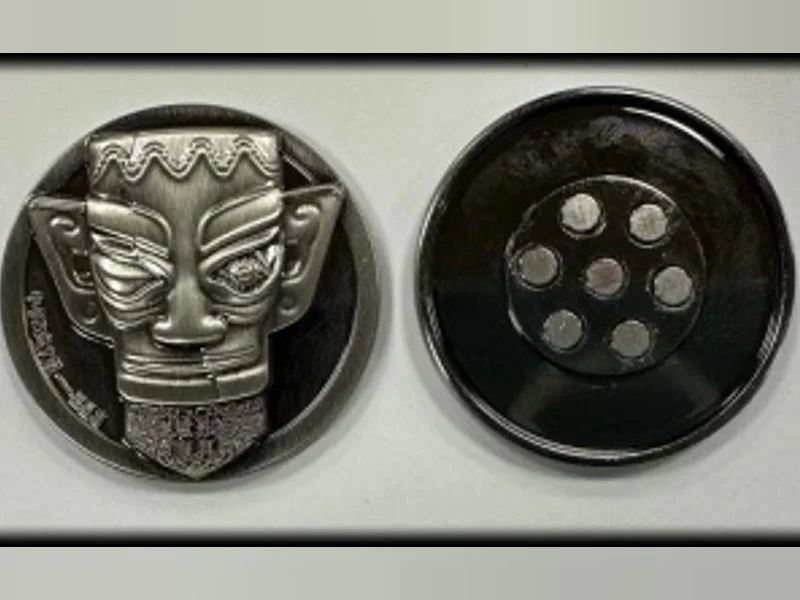
Over 70 of our die-cast Zamak #3 sliders and coins in our Magnetic Fidget Sliders and Haptic Fidget Coins collections feature intricate 3D relief artwork—such as FS-001 (Poker King), FS-010 (Gothic Skull), FS-017 (Ancient Bronze Mask Coin), and FS-024 (Royal King/Queen).
If you plate a 3D sculpture in uniform bright chrome, glare washes out all the fine engraving detail. Instead, our electroplating line executes a 4-stage museum-grade relieved antique process:
- Alkaline Copper + Semi-Bright Nickel Base (
12 microns): Seals the die-cast zinc substrate and creates a metallurgical diffusion barrier. - Electrochemical Bronze / Silver / Gunmetal Deposit: Plates the true metallic color layer across all peaks and valleys.
- Chemical Patination & Hand Cotton-Wheel Relieving: The shell is immersed in an oxidizing bath to turn the entire surface dark espresso/charcoal, then hand-buffed on a soft sisal/cotton wheel. The wheel buffs away the dark oxide only on the raised 3D highlights, leaving deep dark shadows inside the recessed grooves for dramatic chiaroscuro depth!
- Cathodic Electrophoretic Clear Coat (
E-CoatBaked at160°C): Seals the relieved patina beneath an invisible, sweat-proof polyurethane-acrylic film that prevents green copper verdigris or finger tarnish.
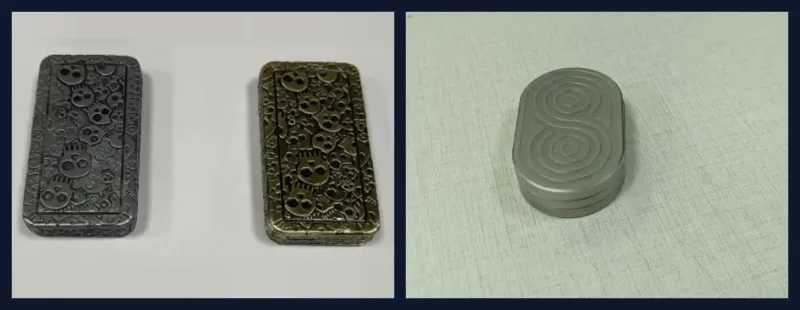
4. Ceramic Stonewashing vs. Vacuum PVD on 304/316 CNC Stainless Steel
For premium models in our CNC Stainless Steel & Exotic Metals collection (FS-013, FS-063, FS-075, FS-086, FS-120), buyers typically choose between two zero-peel finishes:
- Isotropic Ceramic Media Stonewashing (Tumbled Matte): After 5-axis CNC milling, stainless steel parts are tumbled for 4 hours inside rotary barrels filled with
4mmtriangular porcelain-ceramic media and mild surfactant. The ceramic pyramids micro-peen every corner (R0.3mmchamfer), erasing CNC toolpath marks and creating an organic, non-directional matte patina that never shows fingerprints or pocket scratches. - Vacuum Magnetron Sputtering PVD (Physical Vapor Deposition): Inside a high-vacuum chamber (
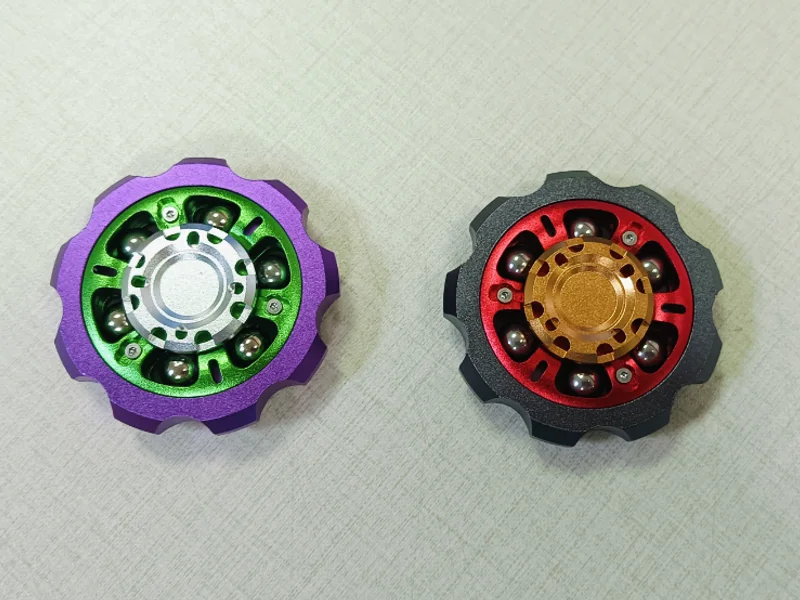
10⁻⁴ Paat350°C), vaporized titanium, zirconium, or carbon ions bond atomically to the stainless steel surface—producing Matte Black DLC, Gold TiN, or Iridescent Oil-Slick Rainbow (FS-120) with a surface hardness of2,000+ HV(harder than quartz sand).
5. How Surface Finish Dictates Custom Logo Contrast (Laser vs. Silk-Screen vs. Color Fill)
Before selecting a custom branding method from our Laser Engraving vs. Silk-Screen & Color Fill Guide, match your chosen surface finish to the optimal marking physics:
| Surface Finish | 50W Fiber Laser Result | Silk-Screen / Deep Color Fill Result | Best Branding Recommendation |
|---|---|---|---|
| Anodized 6063 Aluminum (Black / Blue / Red) | 10/10 Contrast — Laser bleaches dye to crisp chalk-white $\text{Al}_2\text{O}_3$ | 9/10 — Smooth matte pores bond tightly with screen ink | Standard 50W Fiber Laser Engraving (+$0.15–$0.30/pc) |
| Matte Black / Dark Gunmetal PVD | 10/10 Contrast — Vaporizes dark PVD to reveal bright silver steel | 9/10 — Ideal for metallic gold/white silk-screen logos | Fiber Laser Engraving or Gold Silk-Screen Print |
| Stonewashed / Brushed Raw 304 Stainless | 9/10 Contrast — Dark-annealing laser pulse creates charcoal-black oxide mark | 10/10 Contrast with Deep Laser + Baked Enamel Color Fill | Dark Annealing Fiber Laser or Deep Laser + Color Fill |
| Relieved Antique Bronze / Silver | 8.5/10 — Subtle tone-on-tone engraved hallmark on back/track plate | 9.5/10 — Bright opaque Silk-Screen pops against dark antique base | Multi-Color Silk-Screen Print or Deep Laser + Color Fill |
6. Custom Pantone Anodizing / Plating Runs & RoHS 3 / EN 1811 Nickel Compliance
All five surface finishing lines at our factory strictly comply with EU RoHS 3, REACH SVHC, California Prop 65, and EN 1811 skin-contact nickel-release limits (see our US CPSC & EU RoHS/REACH Compliance Guide). Need a custom brand color? At a 300-piece MOQ, we can dye anodized aluminum to your exact Pantone swatch or run custom PVD/antique tones—paired with sulfur-free EVA foam packaging (Custom EVA & Tin Box Packaging Guide).
Quality Control Testing Protocol: Cross-Hatch Adhesion (ASTM D3359) & Artificial Sweat Immersion (ISO 3160-2)
Before any electroplated, anodized, or PVD-coated production batch is cleared for final magnet assembly at our Dongguan plant, our surface-metallurgy QC laboratory pulls 5 sample shells per 500-piece lot for destructive and non-destructive coating verification. Using an X-ray fluorescence (XRF) coating thickness analyzer, technicians verify that copper-nickel base layers exceed 12 microns and anodic oxide layers exceed 18 microns. Next, samples undergo an ASTM D3359 cross-hatch tape adhesion test (scoring a 1mm × 1mm lattice into the finish and pulling with high-tack pressure-sensitive tape to verify 5B zero-flaking adhesion) followed by a 24-hour ISO 3160-2 artificial human sweat immersion bath at 40°C—guaranteeing that your customers never experience green finger staining, clear-coat delamination, or premature finish fade.
Order Our 5-Finish Surface Metallurgy Swatch & Sample Kit
Want to inspect Vacuum Rainbow PVD (FS-120), Bead-Blasted Hard Anodized Aluminum (FS-047), Ceramic Stonewashed 304SS (FS-086), and Relieved Antique Bronze (FS-001) in person? Contact our engineering desk today.
Request 5-Finish Sample Kit & Quote →